High Quality PUL Fabric - Waterproof, Safe, and Built to Last

application/high-quality-pul-fabric, application/high-quality-pul-fabric, 
Get a Quote
application/high-quality-pul-fabric, application/high-quality-pul-fabric, 
Get a Quote

high quality pul fabric

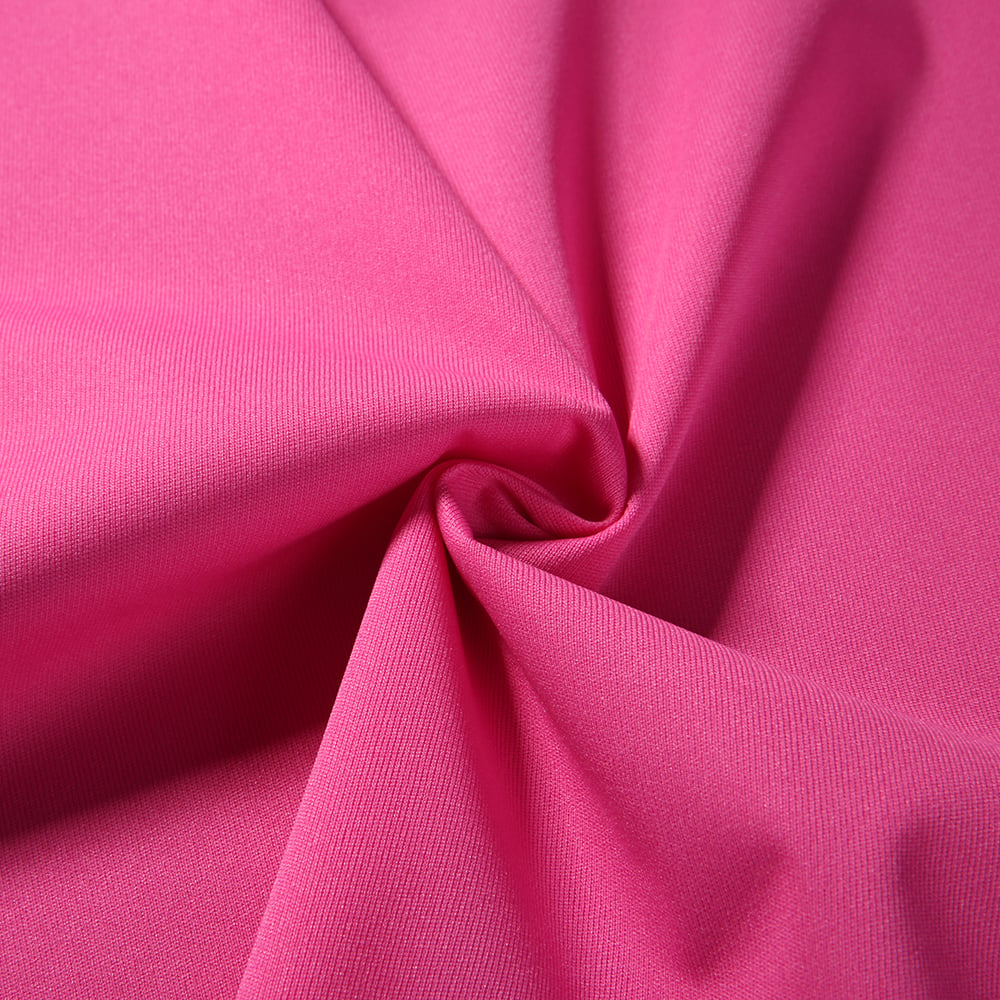
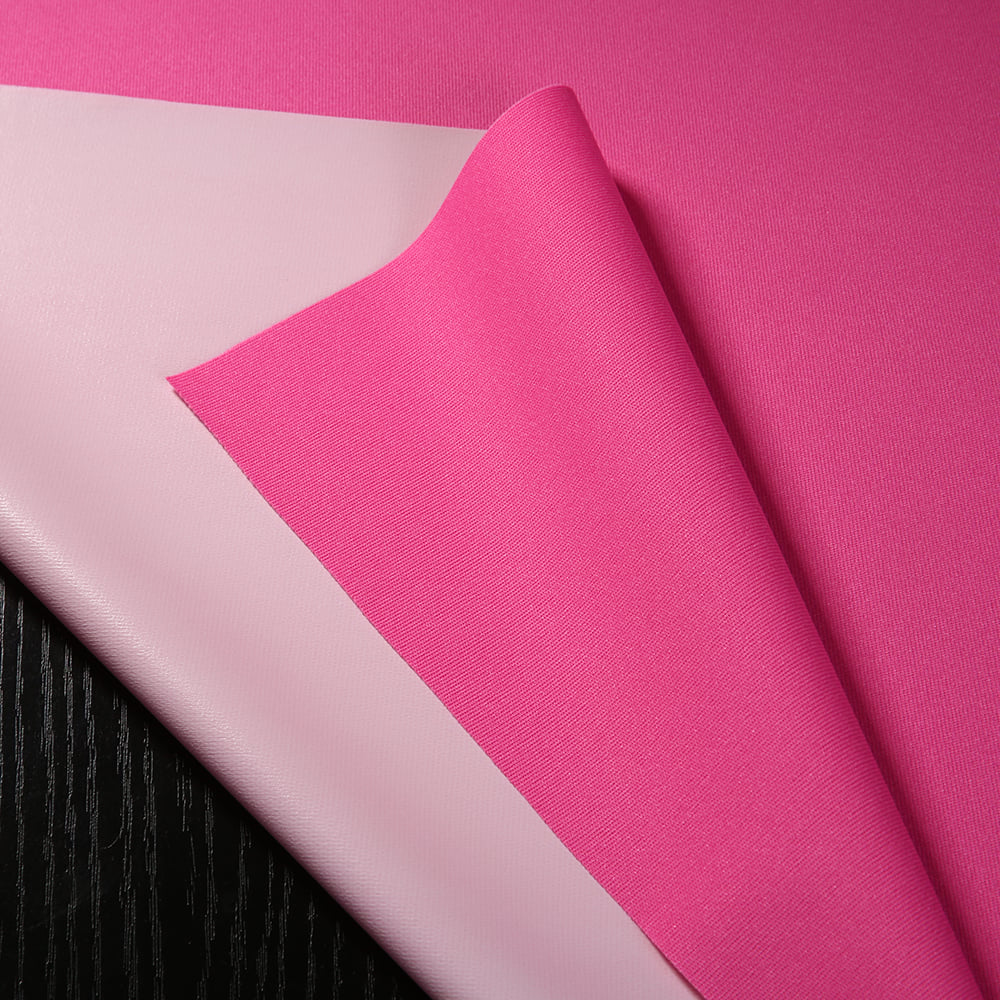
High quality PUL fabric stands at the forefront of modern textile engineering, combining advanced polymer science with practical everyday functionality. PUL, which stands for polyurethane laminate, is a two-layer or three-layer composite material that bonds a thin polyurethane film to a woven or knitted base fabric, typically polyester or cotton. The result is a textile that delivers outstanding waterproof performance while retaining a soft, flexible hand feel that makes it comfortable against the skin and easy to work with during manufacturing and crafting. The core function of high quality PUL fabric is to create a reliable moisture barrier. Unlike coated fabrics that can crack, peel, or stiffen over time, the laminated construction of high quality PUL fabric ensures the waterproof layer remains bonded through repeated washing, stretching, and daily use. This durability is a direct result of the heat-bonding or adhesive lamination process used during production, which fuses the polyurethane membrane uniformly across the entire surface of the base fabric. From a technological standpoint, high quality PUL fabric is engineered to meet specific performance benchmarks. The polyurethane layer is typically between 1 mil and 2 mil in thickness, providing a balance between flexibility and barrier strength. Many versions of high quality PUL fabric are certified to meet safety standards such as OEKO-TEX Standard 100, confirming that the material is free from harmful substances and safe for use in products that come into direct contact with sensitive skin, including infant and baby items. The applications of high quality PUL fabric span a wide range of industries and consumer products. In the baby care sector, it is the material of choice for reusable cloth diapers, diaper covers, and waterproof changing pads. In healthcare, it is used for incontinence products, medical bed pads, and protective garments. Outdoor and sportswear brands rely on high quality PUL fabric for rain gear, waterproof bags, and protective covers. Crafters and small-scale manufacturers also use it extensively for wet bags, swimwear liners, and custom waterproof accessories. Its combination of safety, durability, and versatility makes high quality PUL fabric one of the most trusted materials across multiple sectors worldwide.
When you choose high quality PUL fabric for your products or projects, you are making a practical decision that pays off in multiple ways. Here is a clear breakdown of the real-world benefits that this material delivers to customers, manufacturers, and end users alike. First, high quality PUL fabric keeps moisture exactly where it belongs. Whether you are making a reusable diaper, a wet bag, or a waterproof mattress cover, the polyurethane laminate layer stops liquid from passing through. This is not a temporary coating that wears off after a few washes. The laminate is bonded directly into the fabric structure, so it holds up wash after wash without losing its waterproof properties. You get consistent protection every single time you use the product. Second, high quality PUL fabric is remarkably soft and flexible. Many waterproof materials feel stiff, crinkly, or uncomfortable against the skin. High quality PUL fabric solves this problem by using a soft knit or woven base that moves naturally with the body. This makes it ideal for items worn close to the skin, such as cloth diapers, period underwear liners, and incontinence pads. The softness also makes it much easier to cut, sew, and assemble during production, reducing manufacturing time and material waste. Third, high quality PUL fabric is built to last. Products made from this material can withstand hundreds of machine wash cycles without degrading. The laminate does not crack, peel, or delaminate under normal use conditions. This long service life translates directly into cost savings for the customer. Instead of replacing disposable waterproof products repeatedly, a single item made from high quality PUL fabric can serve reliably for years. Fourth, high quality PUL fabric is available in a wide range of colors, prints, and weights, giving designers and manufacturers enormous creative flexibility. You can source it in solid colors for medical and professional applications, or in vibrant prints for baby products and consumer goods. This versatility means you do not have to compromise on aesthetics to get the performance you need. Fifth, high quality PUL fabric meets rigorous safety standards. Many certified versions are tested and approved under OEKO-TEX Standard 100, meaning they contain no harmful dyes, chemicals, or residues. This is especially important for products used by infants, young children, or people with sensitive skin. Choosing a certified high quality PUL fabric gives both manufacturers and consumers confidence that the material is safe for direct skin contact. Sixth, high quality PUL fabric supports sustainable product design. Because it enables the creation of reusable, long-lasting products, it directly reduces the volume of single-use disposable items that end up in landfills. For brands focused on environmental responsibility, building products with high quality PUL fabric is a straightforward way to reduce waste and appeal to eco-conscious consumers. In summary, high quality PUL fabric delivers waterproof reliability, lasting durability, skin-friendly softness, design flexibility, certified safety, and environmental value all in one material. These are not abstract claims but practical advantages that show up in the performance and longevity of every product made with it.

Practical Tips

What is TPU?

11

Aug

What is TPU?

View More
Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

13

Mar

Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

View More
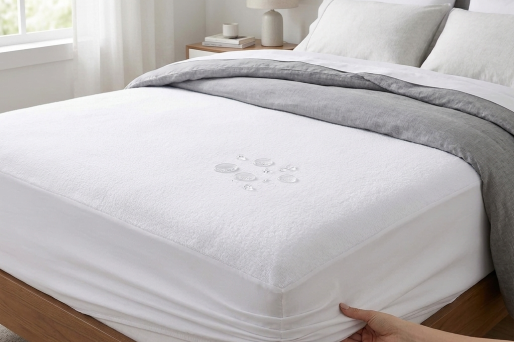
Bamboo vs. Cotton vs. Lyocell: Which Waterproof Mattress Protector Top Layer Is Right for You?

05

Aug

Bamboo vs. Cotton vs. Lyocell: Which Waterproof Mattress Protector Top Layer Is Right for You?

View More
Fitted Sheet vs. Zippered Encasement: Which One Should You Choose?

22

May

Fitted Sheet vs. Zippered Encasement: Which One Should You Choose?

View More

Get a Free Quote

Our representative will contact you soon.
0/1000
Unmatched Waterproof Performance That Lasts

Unmatched Waterproof Performance That Lasts

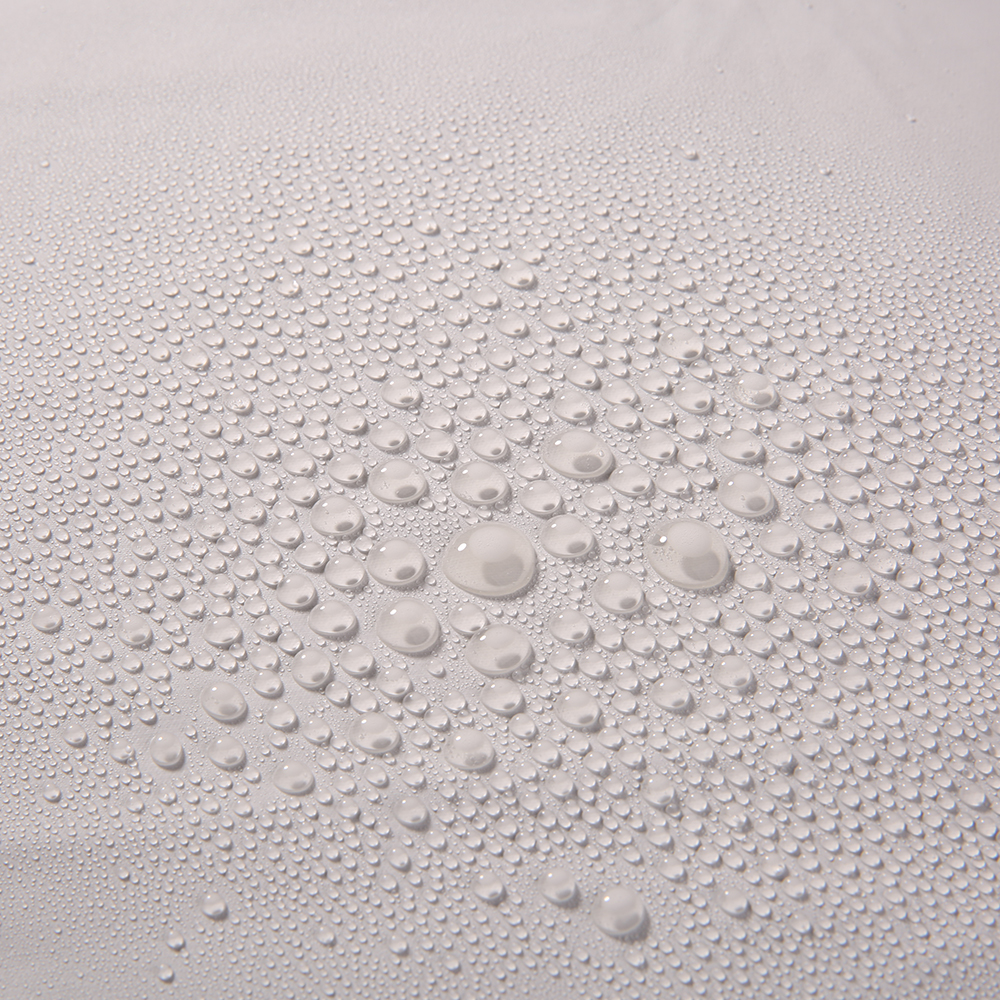
The most important reason professionals and consumers choose high quality PUL fabric is its ability to deliver consistent, long-lasting waterproof protection. Understanding why this matters requires looking at how the material is constructed and how it performs compared to alternatives. The polyurethane laminate in high quality PUL fabric is not a surface coating applied on top of the fabric. It is a thin, flexible film that is thermally bonded or adhesive-laminated directly to the base fabric at the molecular level. This bonding process creates a uniform, continuous barrier across the entire surface of the material. There are no gaps, thin spots, or weak points where moisture can seep through. When liquid contacts the surface of high quality PUL fabric, it cannot penetrate the laminate layer. It beads up and rolls off, or it is contained on one side of the fabric without transferring to the other. This is the fundamental property that makes high quality PUL fabric the preferred choice for products where leakage is simply not acceptable. Consider the demands placed on a reusable cloth diaper. It must contain liquid reliably for hours at a time, survive being washed at high temperatures dozens of times per month, and remain flexible and comfortable against a baby's skin throughout its entire service life. High quality PUL fabric meets all of these demands simultaneously. Independent testing has shown that properly manufactured high quality PUL fabric retains its waterproof integrity through 200 or more machine wash cycles when cared for according to standard guidelines. This performance durability is what separates high quality PUL fabric from cheaper laminated alternatives that begin to delaminate or develop leaks after only a few dozen washes. The waterproof performance of high quality PUL fabric also holds up under physical stress. The laminate layer is engineered to stretch and recover along with the base fabric, so it does not crack or separate when the material is pulled, folded, or compressed during use. This flexibility under stress is critical for applications like fitted diaper covers, form-fitting medical garments, and waterproof bags that are regularly packed and unpacked. For manufacturers, the consistent waterproof performance of high quality PUL fabric means fewer product defects, lower return rates, and stronger customer satisfaction. For end users, it means genuine peace of mind knowing that the product will perform as expected every single time. This reliability is the foundation of the trust that high quality PUL fabric has earned across the baby care, healthcare, outdoor, and crafting industries over many years of proven use.
Certified Safety for Sensitive Skin and Vulnerable Users

Certified Safety for Sensitive Skin and Vulnerable Users

Safety is not a feature that can be assumed in textile manufacturing. It must be tested, verified, and certified by independent bodies before any responsible manufacturer can make safety claims about their materials. High quality PUL fabric earns its reputation for safety through rigorous third-party testing and compliance with internationally recognized standards. The most widely referenced certification for high quality PUL fabric is OEKO-TEX Standard 100. This certification requires that every component of the fabric, including the base textile, the polyurethane laminate, and any dyes or finishing agents used in production, be tested for a comprehensive list of harmful substances. These include heavy metals, formaldehyde, pesticide residues, allergenic dyes, and pH levels that could irritate skin. A fabric that carries OEKO-TEX Standard 100 certification has passed all of these tests and has been confirmed safe for direct skin contact. For high quality PUL fabric used in baby products, the certification standard is even more stringent. Products classified for use by infants and young children must meet the tightest limits for every tested substance, reflecting the greater vulnerability of young skin and the likelihood of prolonged direct contact. When a manufacturer sources certified high quality PUL fabric for cloth diapers, baby blankets, or changing pads, they are providing documented assurance to parents that the material touching their child's skin has been independently verified as safe. This matters enormously in a market where parents are increasingly informed and concerned about the chemical content of products used for their children. Beyond infant care, the safety profile of high quality PUL fabric is equally important in healthcare settings. Incontinence products, medical bed pads, and protective garments made from high quality PUL fabric come into prolonged contact with patients who may have compromised skin integrity or heightened sensitivity. Using a certified, skin-safe material in these applications is not just a quality preference but a clinical responsibility. The safety advantages of high quality PUL fabric also extend to the manufacturing environment. Because the lamination process used in producing high quality PUL fabric does not rely on solvent-based coatings or toxic finishing chemicals, the production process is cleaner and safer for workers. This aligns with the growing demand from brands and retailers for supply chain transparency and responsible manufacturing practices. Choosing high quality PUL fabric means choosing a material whose safety credentials are documented, verifiable, and backed by independent science rather than marketing claims alone.
Versatile Applications Across Industries and Creative Projects

Versatile Applications Across Industries and Creative Projects

One of the most compelling qualities of high quality PUL fabric is the sheer breadth of applications it supports. Few materials can move seamlessly from a hospital supply room to a baby nursery to an outdoor adventure gear workshop while maintaining the same high standard of performance in each context. This versatility is a direct result of the material's unique combination of properties. In the baby and childcare market, high quality PUL fabric is the backbone of the reusable diaper industry. Diaper covers, all-in-one diapers, pocket diapers, and swim diapers all rely on high quality PUL fabric to provide the waterproof outer layer that keeps clothing and bedding dry. Beyond diapers, it is used for waterproof changing pads, wet bags for storing soiled items while traveling, and waterproof bibs. The ability to wash and reuse these products hundreds of times without degradation makes high quality PUL fabric the economically and environmentally superior choice over disposable alternatives. In healthcare and elder care, high quality PUL fabric serves critical protective functions. Waterproof mattress covers and bed pads protect against incontinence-related moisture damage. Reusable incontinence briefs and pads use high quality PUL fabric as the outer barrier layer. Protective aprons and garments for medical staff are constructed from it to provide reliable fluid resistance during procedures. The washability and durability of high quality PUL fabric make it far more cost-effective than disposable protective products in institutional settings where large volumes are used daily. The outdoor and sportswear industry uses high quality PUL fabric for rain jackets, waterproof stuff sacks, dry bags, and protective equipment covers. Its lightweight nature and flexibility make it suitable for packable gear where bulk and weight are concerns. Crafters and independent designers have embraced high quality PUL fabric as a go-to material for handmade waterproof accessories, including cosmetic bags, swimwear liners, reusable snack bags, and custom wet bags. The wide availability of high quality PUL fabric in diverse colors and prints means that functional waterproof products do not have to sacrifice visual appeal. This versatility across professional, medical, outdoor, and creative applications confirms that high quality PUL fabric is not a niche specialty material but a broadly useful textile that solves real waterproofing challenges across many different contexts. Its adaptability is one of the primary reasons demand for high quality PUL fabric continues to grow globally.