TPU Coated Fabric - Waterproof & Breathable

application/tpu-coated-fabric, application/tpu-coated-fabric, 
Get a Quote
Get a Quote

tpu coated fabric

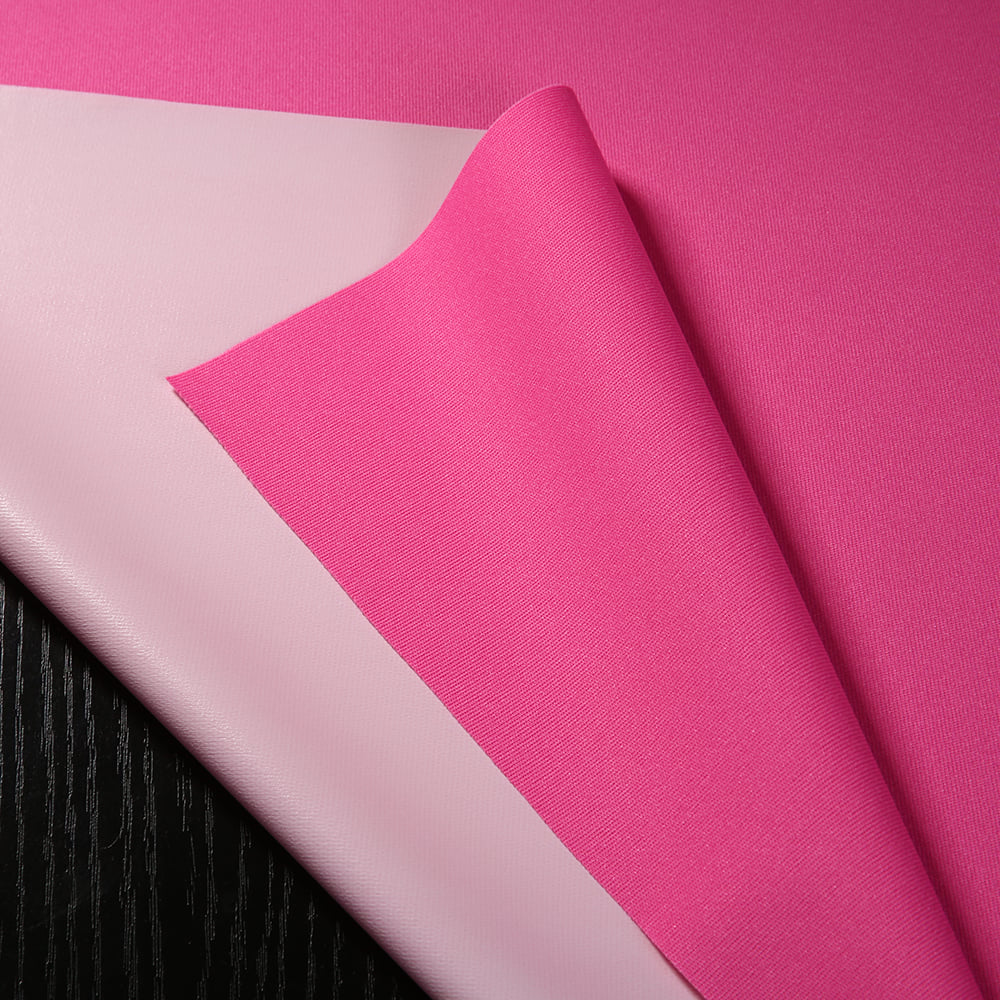
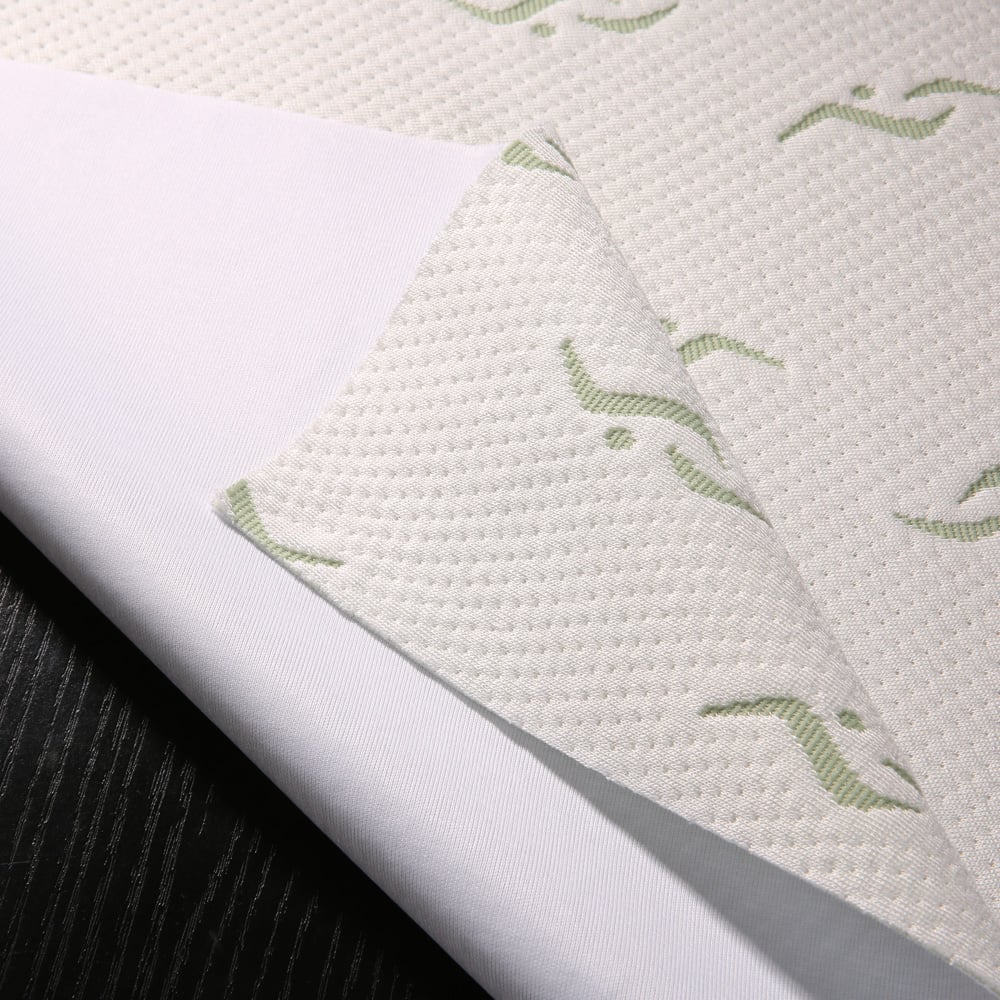
TPU coated fabric represents a revolutionary textile innovation that combines the durability of traditional fabrics with the advanced protective properties of thermoplastic polyurethane. This specialized material consists of a base fabric layer, typically polyester or nylon, bonded with a thin TPU film through heat lamination or adhesive processes. The result is a high-performance textile that delivers exceptional waterproofing, breathability, and mechanical strength. TPU coated fabric has emerged as a preferred choice across numerous industries due to its unique combination of flexibility, abrasion resistance, and environmental stability. The thermoplastic polyurethane coating creates an impermeable barrier against water, wind, and contaminants while maintaining the fabric's natural drape and softness. Unlike traditional coating methods, the TPU layer remains elastic and resistant to cracking even in extreme temperatures, ranging from -40 to 90 degrees Celsius. This material finds extensive applications in outdoor apparel, medical textiles, protective equipment, automotive interiors, and technical sportswear. The manufacturing process allows for customization in thickness, transparency, and texture, making TPU coated fabric adaptable to specific performance requirements. Its recyclable nature and reduced environmental impact compared to PVC alternatives have positioned it as a sustainable choice for forward-thinking manufacturers. Whether used in rain jackets, inflatable structures, or medical mattress covers, this versatile textile continues to expand its market presence through continuous technological improvements and innovative applications across diverse sectors.
Choosing TPU coated fabric delivers substantial practical benefits that directly impact product performance and customer satisfaction. The waterproof barrier achieves hydrostatic ratings exceeding 10,000mm, ensuring complete protection against rain, snow, and moisture penetration in demanding conditions. This superior water resistance does not compromise breathability, as the TPU membrane allows water vapor to escape, preventing interior condensation and maintaining user comfort during physical activities. The material demonstrates remarkable durability, withstanding repeated flexing, stretching, and abrasion without degradation, which translates to longer product lifecycles and reduced replacement costs for end users. Unlike rubber or PVC coatings that become stiff and crack over time, TPU coated fabric retains its flexibility and elastic recovery even after years of use and exposure to UV radiation. The lightweight nature of this textile reduces transportation costs and enhances wearability in garments without sacrificing protective capabilities. Manufacturers benefit from easier processing and welding capabilities, as TPU coated fabric can be heat-sealed to create waterproof seams without additional tapes or adhesives. The material resists oils, greases, and most chemicals, making it ideal for industrial and medical applications where contamination control is critical. Its hypoallergenic properties and resistance to microbial growth support hygiene requirements in healthcare settings. The transparent coating options maintain the aesthetic appearance of the base fabric while providing protection, allowing designers to create visually appealing products without functional compromise. Temperature stability ensures consistent performance across seasonal variations, eliminating the brittleness issues common in cold weather applications. The recyclability of TPU coated fabric aligns with corporate sustainability goals and increasingly stringent environmental regulations, providing a responsible choice that appeals to environmentally conscious consumers while meeting performance expectations across diverse applications.

Latest News

What is TPU?

11

Aug

What is TPU?

View More
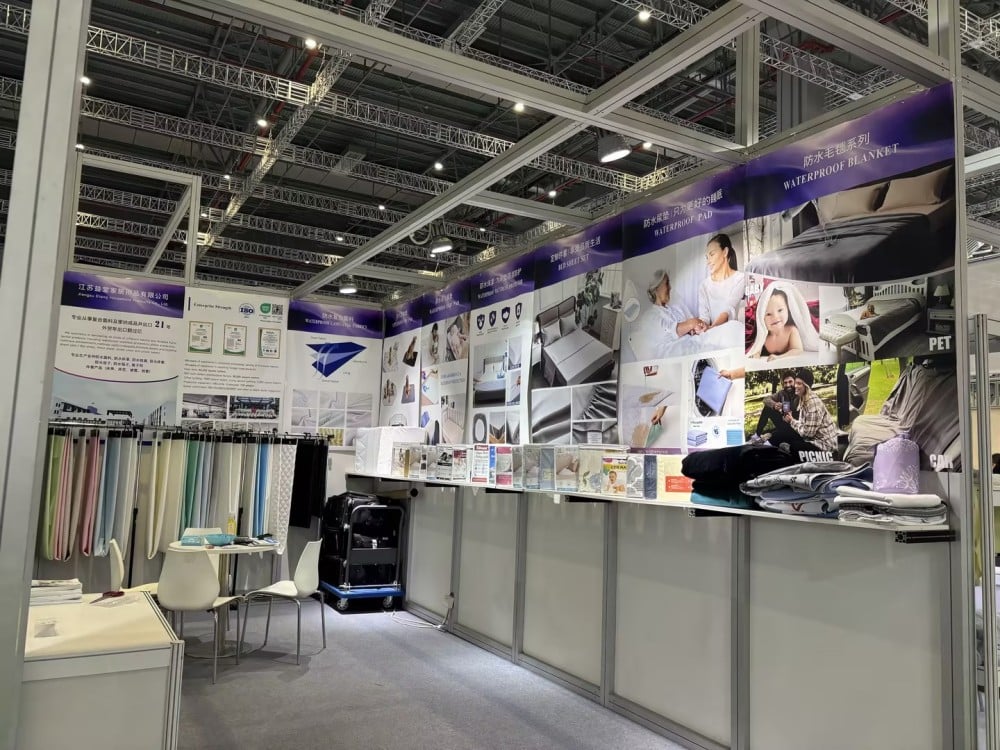
Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

11

Aug

Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

View More
Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

13

Mar

Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

View More
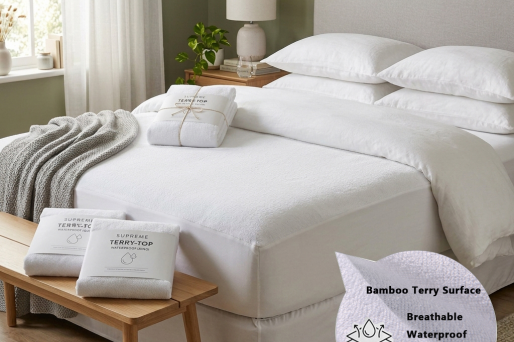
Bamboo Terry Waterproof Mattress Protector: The Cool, Quiet & Leak-Proof Solution

29

Jul

Bamboo Terry Waterproof Mattress Protector: The Cool, Quiet & Leak-Proof Solution

View More

Get a Free Quote

Our representative will contact you soon.
0/1000
Exceptional Waterproof Breathability Balance

Exceptional Waterproof Breathability Balance

TPU coated fabric achieves an optimal balance between complete waterproof protection and breathable comfort that sets it apart from competing materials. The microscopic pore structure within the thermoplastic polyurethane layer blocks liquid water molecules while permitting smaller water vapor molecules to pass through freely. This intelligent permeability creates a microclimate management system that keeps users dry from both external moisture and internal perspiration. During high-intensity activities, the fabric efficiently wicks away body moisture, preventing the clammy discomfort associated with non-breathable waterproof materials. This performance characteristic proves essential in outdoor gear, athletic wear, and occupational protective clothing where extended wear periods demand sustained comfort. The breathability does not diminish the waterproof integrity, as laboratory testing consistently demonstrates hydrostatic head ratings above 10,000mm alongside moisture vapor transmission rates exceeding 5,000 g/m2/24hr. This dual functionality eliminates the traditional trade-off between protection and comfort, delivering comprehensive performance that enhances user experience across varied environmental conditions and activity levels.
Superior Durability and Longevity

Superior Durability and Longevity

The mechanical resilience of TPU coated fabric ensures extended service life that justifies initial investment through reduced replacement frequency and maintenance requirements. The thermoplastic polyurethane coating exhibits exceptional abrasion resistance, withstanding repeated friction against rough surfaces without wearing through or delaminating from the base fabric. This durability proves particularly valuable in high-wear applications such as backpack bottoms, knee reinforcements, and equipment covers that experience constant contact and stress. The material maintains tensile strength exceeding 500N even after prolonged exposure to UV radiation, temperature fluctuations, and chemical contact that would degrade conventional coatings. Flex fatigue testing demonstrates that TPU coated fabric endures over 100,000 flex cycles without cracking, a critical performance metric for articulated joints in garments and repeated folding in storage applications. The elastic memory of the TPU layer allows the fabric to return to its original shape after stretching or compression, preventing the sagging and distortion that compromise both appearance and function over time. This long-term stability translates to reliable performance throughout the product lifecycle, reducing warranty claims and enhancing brand reputation.
Environmentally Responsible Material Choice

Environmentally Responsible Material Choice

TPU coated fabric represents a significant advancement in sustainable textile technology, addressing environmental concerns without compromising performance standards. Unlike PVC-based alternatives that release harmful plasticizers and dioxins during production and disposal, thermoplastic polyurethane contains no toxic heavy metals or chlorinated compounds. The material is fully recyclable through mechanical and chemical processes, allowing end-of-life products to be reprocessed into new applications rather than contributing to landfill waste. Manufacturing TPU coated fabric requires lower processing temperatures compared to other synthetic coatings, reducing energy consumption and carbon emissions during production. The absence of volatile organic compounds in TPU formulations improves workplace safety and eliminates off-gassing concerns in finished products, making it suitable for sensitive applications including children's products and medical devices. The durability and longevity inherent in this material reduce the frequency of product replacement, thereby decreasing overall resource consumption and waste generation. Many TPU coated fabric manufacturers have achieved environmental certifications including Oeko-Tex Standard 100 and bluesign approval, providing third-party verification of ecological responsibility that supports corporate sustainability reporting and consumer transparency requirements.