Waterproof Laminated Fabric Solutions

application/waterproof-laminated-fabric, application/waterproof-laminated-fabric, 
Get a Quote
application/waterproof-laminated-fabric, application/waterproof-laminated-fabric, 
Get a Quote

waterproof laminated fabric

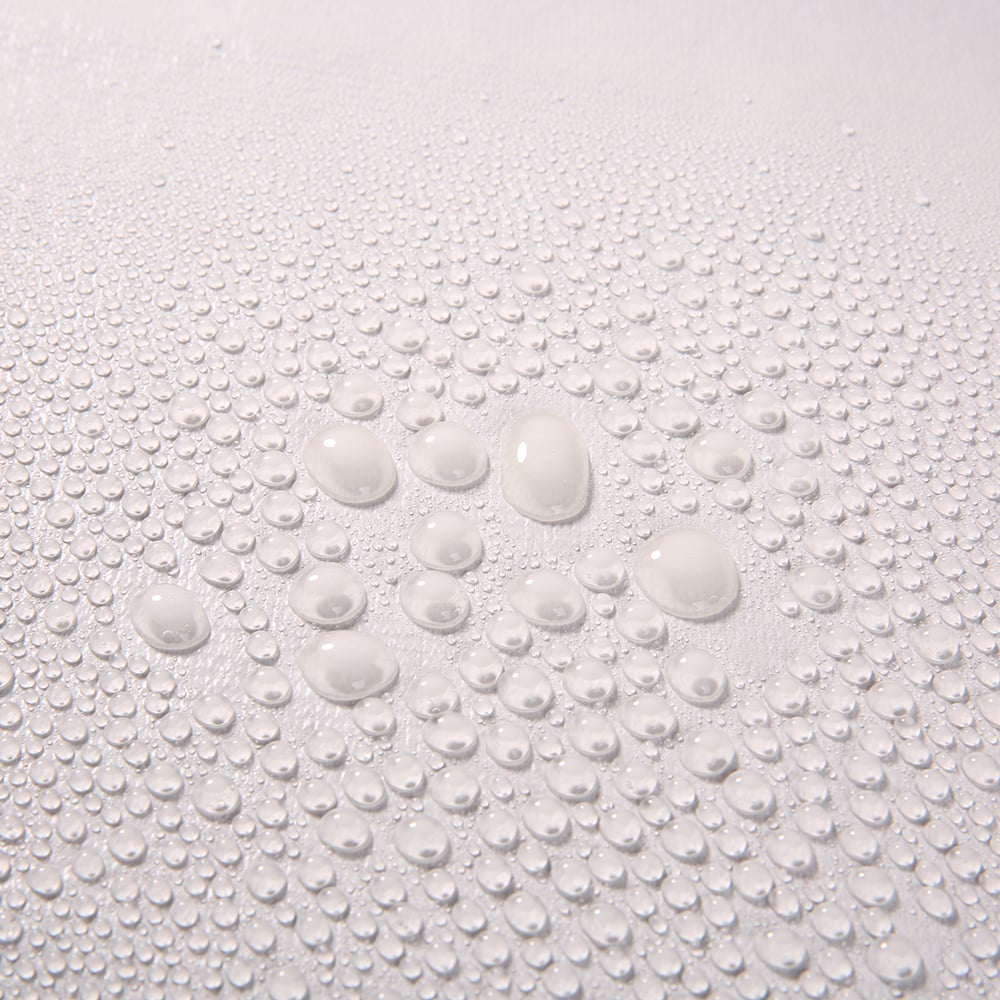
Waterproof laminated fabric represents an advanced textile solution engineered to provide superior moisture protection while maintaining breathability and durability. This innovative material consists of multiple layers bonded together through specialized lamination processes, creating a barrier that prevents water penetration while allowing vapor transmission. The core structure typically includes a base fabric layer, a waterproof membrane, and sometimes an additional protective layer, all seamlessly integrated to deliver exceptional performance. Waterproof laminated fabric utilizes cutting-edge technology such as polyurethane or polytetrafluoroethylene membranes that create microscopic pores small enough to block liquid water molecules yet large enough to permit water vapor escape. This intelligent design ensures wearers stay dry from external moisture while preventing internal condensation buildup. The technological features of waterproof laminated fabric include high hydrostatic pressure resistance, excellent tear strength, and flexibility that maintains performance across varying temperatures. Manufacturing processes employ heat bonding, adhesive lamination, or flame lamination techniques to ensure permanent layer adhesion without compromising fabric integrity. Applications span diverse industries including outdoor apparel, protective workwear, medical textiles, military gear, camping equipment, footwear, and automotive components. The fabric excels in environments demanding reliable moisture protection combined with comfort and longevity. Whether facing torrential rain, snow, or high-humidity conditions, waterproof laminated fabric delivers consistent protection that meets rigorous industry standards and user expectations for quality performance.
Choosing waterproof laminated fabric delivers tangible benefits that directly impact your comfort, safety, and product longevity. The primary advantage lies in its exceptional moisture barrier that keeps you completely dry during extended exposure to wet conditions, eliminating the discomfort and health risks associated with dampness. Unlike traditional coated fabrics that trap perspiration, this advanced material allows body moisture to escape, preventing that clammy feeling during physical activity. This breathability advantage means you remain comfortable whether working outdoors, hiking mountain trails, or engaging in high-intensity activities. The durability of waterproof laminated fabric translates to superior value over time, as the bonded layers resist delamination, cracking, and performance degradation that plague inferior alternatives. You invest once and enjoy years of reliable protection without frequent replacements. The fabric maintains flexibility even in cold temperatures, ensuring garments and products remain functional across seasons and climates. Operational benefits include easy maintenance, as most waterproof laminated fabric resists staining and cleans effortlessly with simple washing procedures. This practical advantage saves time and preserves appearance throughout the product lifecycle. Application suitability extends beyond outdoor recreation to professional environments where workers need dependable protection from chemical splashes, bodily fluids, or harsh weather without sacrificing mobility. The lightweight nature of modern waterproof laminated fabric means protection no longer requires heavy, restrictive materials that limit movement and cause fatigue. Decision-makers appreciate that products made with waterproof laminated fabric meet stringent safety certifications and environmental standards, supporting compliance requirements while delivering performance users demand. The combination of protection, comfort, durability, and versatility makes waterproof laminated fabric the intelligent choice for applications where moisture management directly affects outcomes and satisfaction.

Tips And Tricks

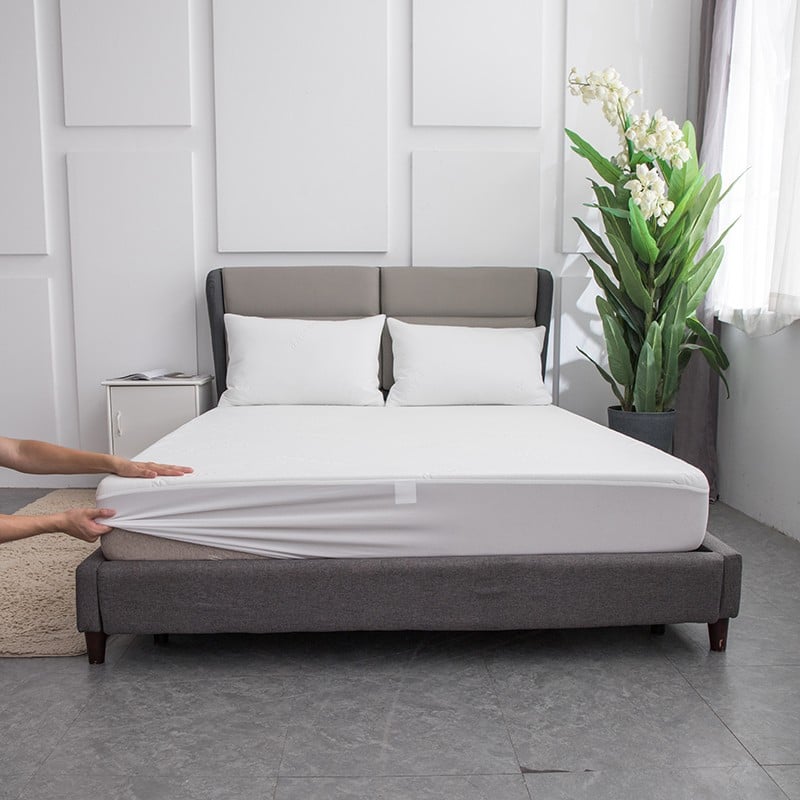
Safe Sleep, Pure Protection: OEKO-TEX® Certified Waterproof Mattress Cover

18

Aug

Safe Sleep, Pure Protection: OEKO-TEX® Certified Waterproof Mattress Cover

View More
What is TPU?

11

Aug

What is TPU?

View More
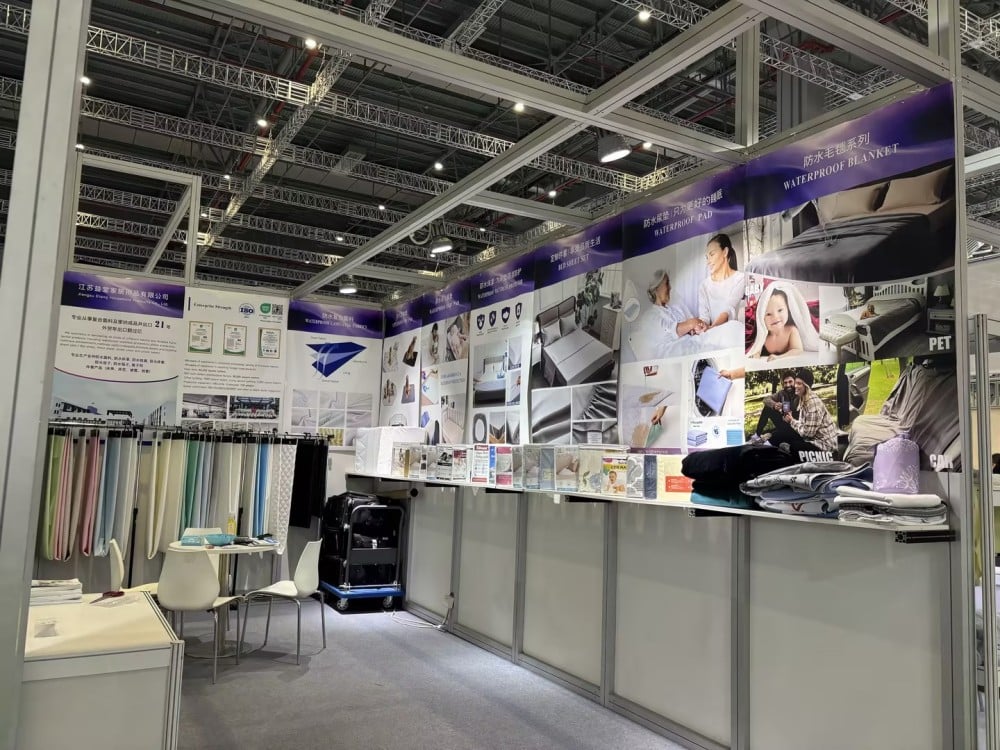
Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

11

Aug

Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

View More
Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

13

Mar

Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

View More

Get a Free Quote

Our representative will contact you soon.
0/1000
Advanced Multi-Layer Protection System

Advanced Multi-Layer Protection System

The sophisticated construction of waterproof laminated fabric sets it apart from conventional water-resistant materials through its engineered multi-layer architecture. Each layer serves a specific protective function, working synergistically to create an impenetrable moisture barrier while maintaining essential breathability. The outer layer provides abrasion resistance and repels initial water contact, the membrane core blocks liquid penetration at the molecular level while permitting vapor transmission, and the inner layer offers comfort and protects the membrane from oils and contaminants. This intelligent layering system ensures waterproof laminated fabric performs consistently under extreme conditions where single-layer materials fail. The lamination process creates permanent bonds between layers, eliminating the risk of separation that compromises protection over time. Advanced manufacturing techniques ensure uniform thickness and consistent performance across every square inch of fabric, providing reliability you can depend on. This comprehensive protection system means products made with waterproof laminated fabric maintain their defensive capabilities through countless wear cycles, temperature fluctuations, and mechanical stress, delivering unmatched longevity and value that justifies the investment for both manufacturers and end users seeking premium performance.
Optimal Breathability Without Compromising Protection

Optimal Breathability Without Compromising Protection

Waterproof laminated fabric solves the traditional dilemma of choosing between complete water protection and adequate ventilation through innovative membrane technology. The microscopic pore structure allows water vapor molecules from perspiration to escape while blocking larger liquid water droplets from penetrating inward. This critical balance maintains internal comfort by preventing moisture accumulation that leads to discomfort, chilling, and reduced performance during physical exertion. The breathability of waterproof laminated fabric significantly outperforms rubber, vinyl, or heavily coated alternatives that trap body heat and moisture, creating uncomfortable microenvironments. Users experience enhanced comfort during extended wear periods, whether working full shifts in protective gear or enjoying multi-day outdoor adventures. The vapor transmission rate of quality waterproof laminated fabric adapts to activity levels, efficiently managing moisture during high-output activities while maintaining protective integrity during rest periods. This dynamic performance characteristic makes the material ideal for variable-intensity applications where conditions and exertion levels change throughout use. The breathability advantage extends product applications beyond emergency protection to everyday wear scenarios where all-day comfort matters as much as weather defense, expanding market opportunities and user satisfaction across diverse customer segments.
Versatile Performance Across Industries

Versatile Performance Across Industries

The adaptability of waterproof laminated fabric makes it the preferred choice across remarkably diverse applications, from fashion-forward outdoor apparel to critical medical protective equipment. This versatility stems from customizable specifications that tailor performance characteristics to specific industry requirements without sacrificing core protective qualities. Manufacturers can select base fabrics, membrane types, and finishing treatments that optimize the waterproof laminated fabric for particular end uses, whether prioritizing lightweight flexibility for athletic wear, chemical resistance for industrial safety gear, or sterile barrier properties for healthcare applications. The material performs equally well in extreme cold where flexibility remains essential and tropical humidity where breathability becomes critical. This cross-industry applicability provides procurement advantages through standardized material platforms that meet multiple departmental needs within organizations, simplifying supply chains and reducing inventory complexity. Product developers appreciate how waterproof laminated fabric accepts printing, embossing, and laminating with additional functional layers, enabling brand differentiation and enhanced features without compromising moisture protection. The fabric integrates seamlessly with various construction techniques including seam sealing, welding, and traditional sewing, offering manufacturing flexibility that accommodates different production capabilities and design requirements. This remarkable versatility ensures waterproof laminated fabric remains relevant across evolving market demands and emerging applications.