TPU Membrane Laminated Fabric - Waterproof & Durable

application/tpu-membrane-laminated-fabric, application/tpu-membrane-laminated-fabric, 
Get a Quote
application/tpu-membrane-laminated-fabric, application/tpu-membrane-laminated-fabric, 
Get a Quote

tpu membrane laminated fabric

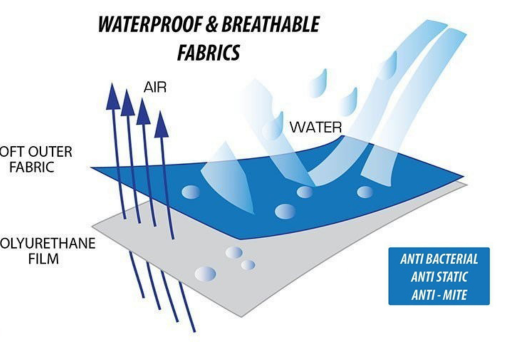
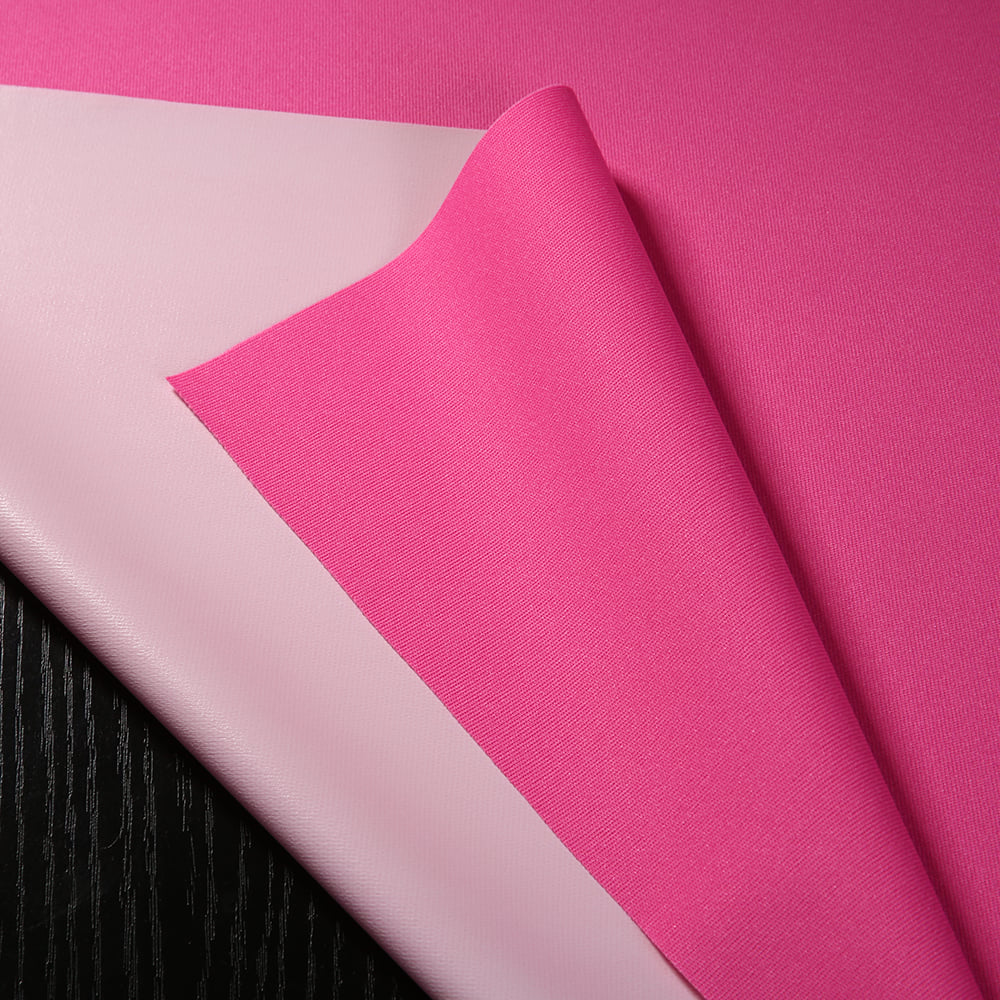
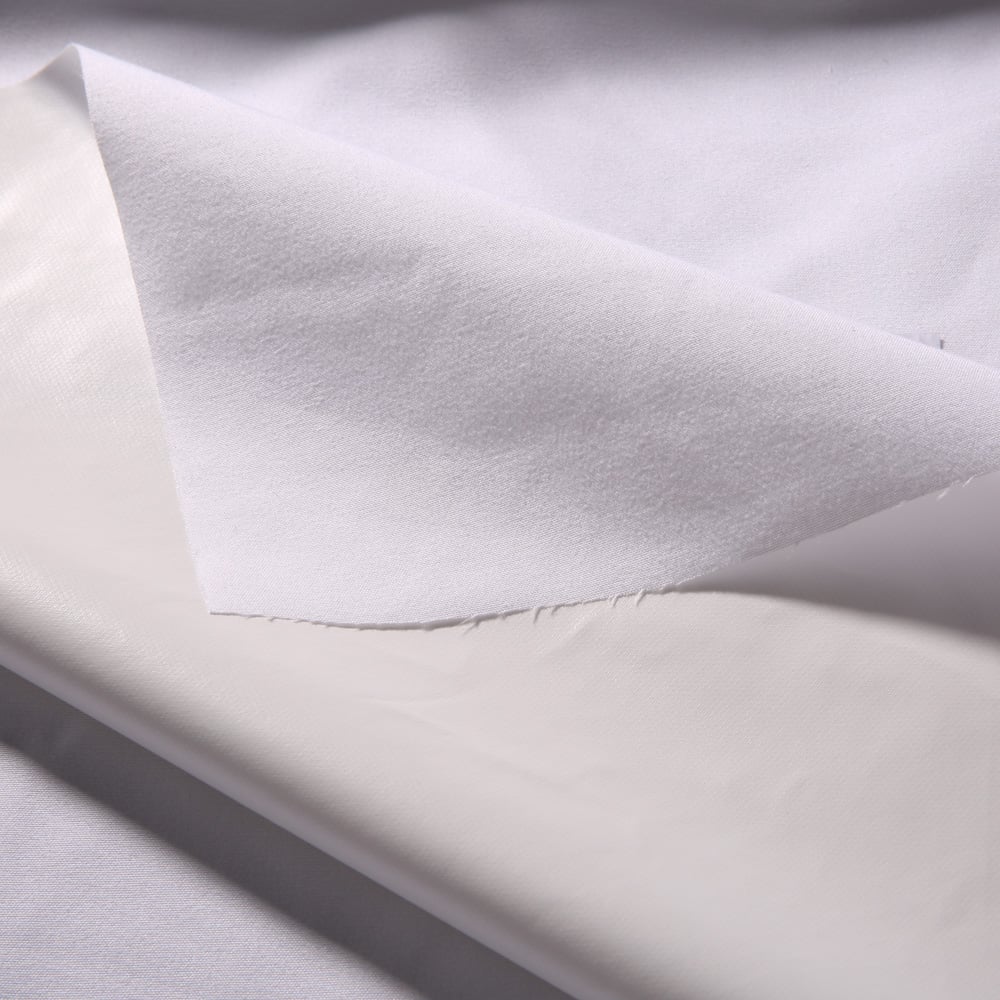
TPU membrane laminated fabric represents an advanced textile solution that combines thermoplastic polyurethane film with various base fabrics through specialized bonding processes. This innovative material delivers exceptional performance characteristics that make it indispensable across multiple industries. The core structure consists of a thin TPU membrane precisely laminated onto textile substrates such as polyester, nylon, or cotton, creating a composite material that retains the comfort and flexibility of traditional fabrics while gaining superior protective properties. The primary functions of TPU membrane laminated fabric include waterproofing, windproofing, and breathability, allowing moisture vapor to escape while preventing water penetration. This three-dimensional protection ensures comfort in demanding conditions. Technologically, the fabric features microscopic pores within the TPU membrane that are small enough to block liquid water droplets yet large enough to permit water vapor molecules to pass through. This intelligent structure maintains an optimal microclimate next to the skin. The lamination process employs heat and pressure to permanently bond the membrane to the fabric without compromising either component's integrity. Applications span outdoor apparel, medical textiles, protective workwear, footwear components, automotive interiors, and technical sporting goods. The versatility of TPU membrane laminated fabric stems from its customizable properties, allowing manufacturers to adjust thickness, breathability levels, and mechanical strength to meet specific performance requirements across diverse end-use scenarios.
Choosing TPU membrane laminated fabric delivers tangible benefits that directly impact product performance and customer satisfaction. The waterproof barrier effectively protects against rain, snow, and moisture while maintaining breathability, preventing the clammy discomfort associated with non-breathable waterproof materials. This dual functionality means users stay dry from both external precipitation and internal perspiration, enhancing comfort during physical activities. The fabric exhibits remarkable durability and abrasion resistance, extending product lifespan and reducing replacement frequency, which translates to better value for investment. Unlike traditional coated fabrics that may crack or delaminate over time, TPU membrane laminated fabric maintains its integrity through repeated washing, flexing, and exposure to environmental stressors. The material remains flexible across wide temperature ranges, performing reliably in both cold and warm conditions without becoming stiff or brittle. This temperature stability makes it suitable for year-round applications and diverse climates. From an operational perspective, the fabric is lightweight compared to rubber or PVC alternatives, reducing material costs in shipping and improving wearing comfort in garments. The material is also more environmentally conscious than many alternatives, as TPU can be recycled and does not release harmful plasticizers. For manufacturers, TPU membrane laminated fabric offers excellent sewability and can be bonded using various sealing techniques to create completely waterproof seams. The aesthetic flexibility allows for multiple color options and finishes, supporting brand differentiation. For end users in outdoor recreation, medical settings, or industrial environments, the fabric provides reliable protection without sacrificing mobility or comfort, making it the practical choice for demanding applications where performance cannot be compromised.

Practical Tips

Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

11

Aug

Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

View More
Unlocking TPU Nanotechnology: Why Your Waterproof Mattress Protector Can Be Leak-Proof and Breathable at the Same Time?

14

May

Unlocking TPU Nanotechnology: Why Your Waterproof Mattress Protector Can Be Leak-Proof and Breathable at the Same Time?

View More
Fitted Sheet vs. Zippered Encasement: Which One Should You Choose?

22

May

Fitted Sheet vs. Zippered Encasement: Which One Should You Choose?

View More
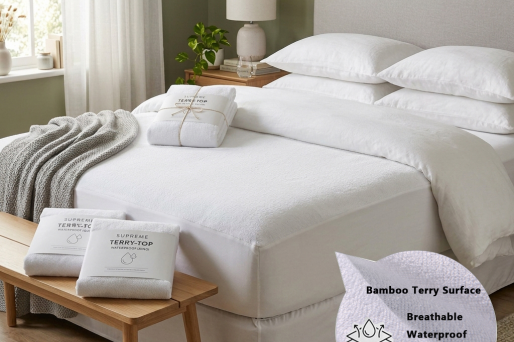
Bamboo Terry Waterproof Mattress Protector: The Cool, Quiet & Leak-Proof Solution

29

Jul

Bamboo Terry Waterproof Mattress Protector: The Cool, Quiet & Leak-Proof Solution

View More

Get a Free Quote

Our representative will contact you soon.
0/1000
Superior Waterproof Breathability Balance

Superior Waterproof Breathability Balance

The defining characteristic of TPU membrane laminated fabric lies in its engineered microporous structure that simultaneously blocks liquid water while allowing water vapor transmission. This seemingly contradictory performance is achieved through precise control of pore size within the TPU membrane layer. Water droplets, being relatively large molecular clusters, cannot penetrate the microscopic pores, creating an effective waterproof barrier that withstands hydrostatic pressures exceeding industry standards. Meanwhile, individual water vapor molecules from perspiration easily pass through these same pores, preventing moisture accumulation inside garments or products. This breathability prevents the build-up of condensation that causes discomfort and reduces thermal efficiency. The result is a fabric that keeps users dry and comfortable across varying activity levels and weather conditions. This balance is particularly valuable in performance apparel where both protection and comfort are non-negotiable requirements. The breathability rate can be customized during manufacturing to suit specific applications, from high-output athletic use requiring maximum vapor transmission to protective equipment prioritizing waterproof integrity. This adaptability makes TPU membrane laminated fabric suitable for specialized professional applications and consumer products alike.
Exceptional Durability and Longevity

Exceptional Durability and Longevity

TPU membrane laminated fabric demonstrates outstanding resistance to the physical stresses that typically degrade textile products over time. The thermoplastic polyurethane membrane possesses inherent elasticity, allowing it to stretch and recover repeatedly without developing cracks or permanent deformation. This elastic memory ensures the fabric maintains its protective properties through thousands of flexing cycles, making it ideal for articulated garment areas like elbows and knees. The lamination bond between membrane and base fabric is engineered to withstand washing, dry cleaning, and environmental exposure without delaminating or bubbling. Abrasion resistance surpasses that of coated fabrics, with the TPU membrane protecting the underlying textile from wear while itself resisting surface degradation. Chemical resistance to oils, greases, and many solvents expands application possibilities into industrial and automotive sectors. UV stability prevents the yellowing and brittleness that affect some plastics, maintaining both appearance and performance during prolonged outdoor exposure. This comprehensive durability profile means products made with TPU membrane laminated fabric require less frequent replacement, delivering economic value through extended service life. For manufacturers, this durability translates to fewer warranty claims and enhanced brand reputation for quality and reliability.
Versatile Processing and Application Flexibility

Versatile Processing and Application Flexibility

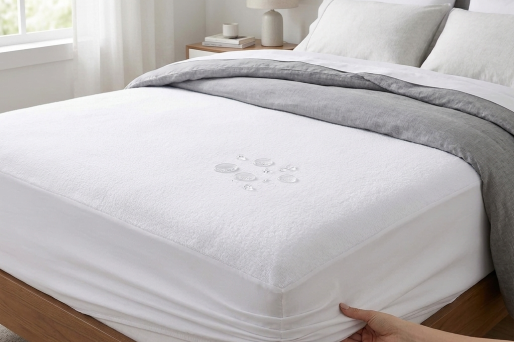
TPU membrane laminated fabric offers remarkable versatility in both manufacturing processes and end-use applications, providing designers and engineers with extensive creative freedom. The material can be laminated to virtually any textile substrate, from lightweight ripstop nylons for ultralight backpacking gear to heavy-duty canvas for industrial applications, allowing performance characteristics to be tailored precisely to intended use. The fabric accepts various finishing treatments including durable water repellent coatings, antimicrobial treatments, and flame retardants, enabling multi-functional performance in a single material. Fabrication methods include traditional sewing, ultrasonic welding, and heat sealing, with the TPU membrane itself serving as an effective adhesive when activated by heat, enabling fully sealed waterproof construction. Printing and embossing techniques can be applied to create branded patterns, textures, or functional surface features. The material's compatibility with standard textile manufacturing equipment minimizes production complexity and cost. Application diversity spans outdoor recreational products, medical mattress covers, protective workwear for hazardous environments, footwear components requiring waterproof breathability, automotive seating that resists spills while remaining comfortable, and countless technical applications. This processing flexibility combined with performance reliability makes TPU membrane laminated fabric a preferred solution when conventional materials cannot meet demanding specifications.