Trusted Underpad Manufacturer: Advanced Absorbent Solutions for Healthcare and Home Care

application/underpad-manufacturer, application/underpad-manufacturer, 
Get a Quote
application/underpad-manufacturer, application/underpad-manufacturer, 
Get a Quote

underpad manufacturer

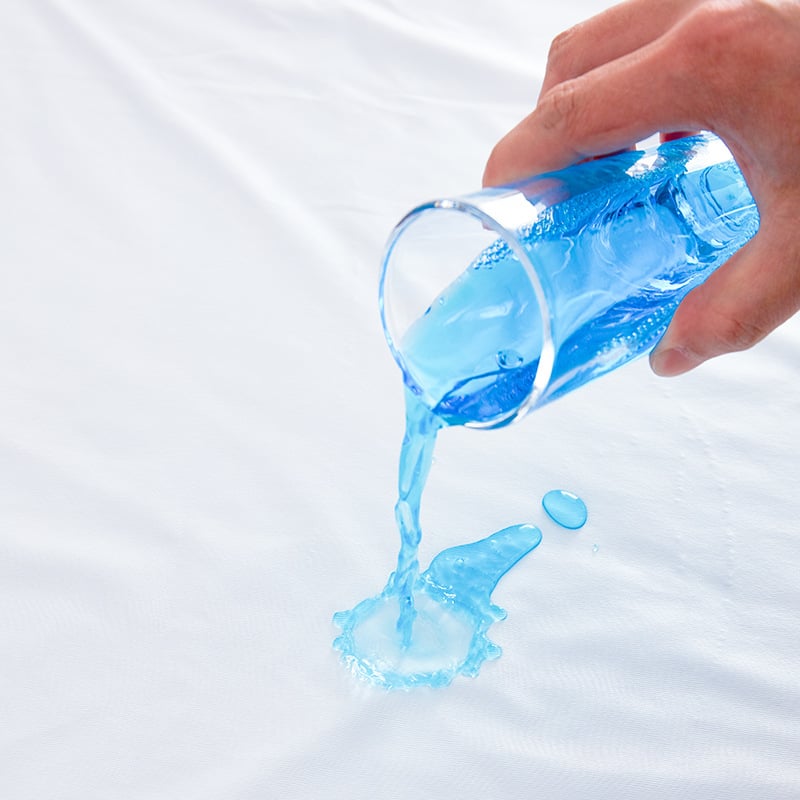
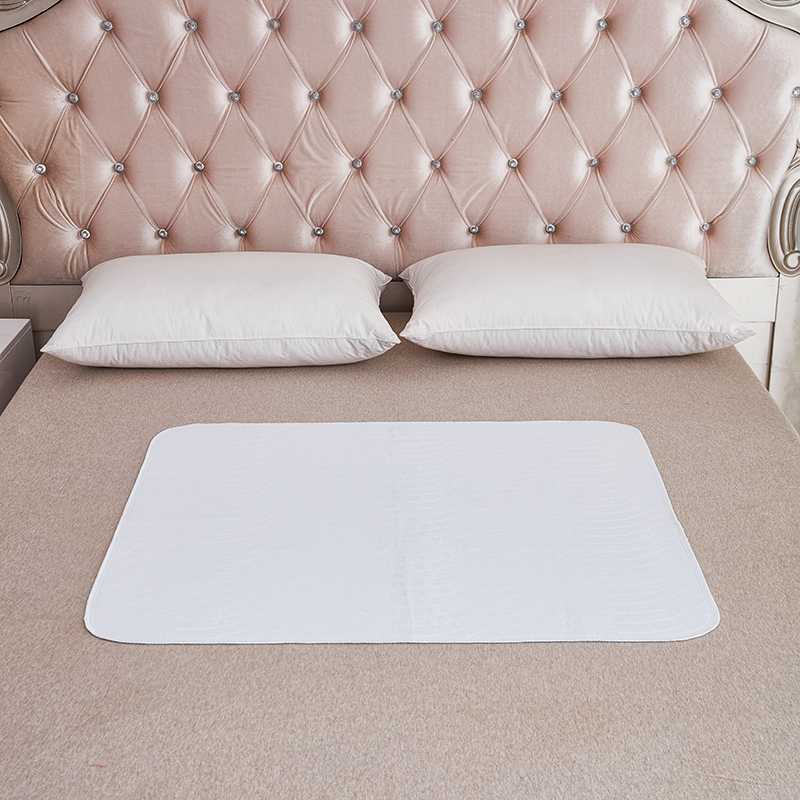
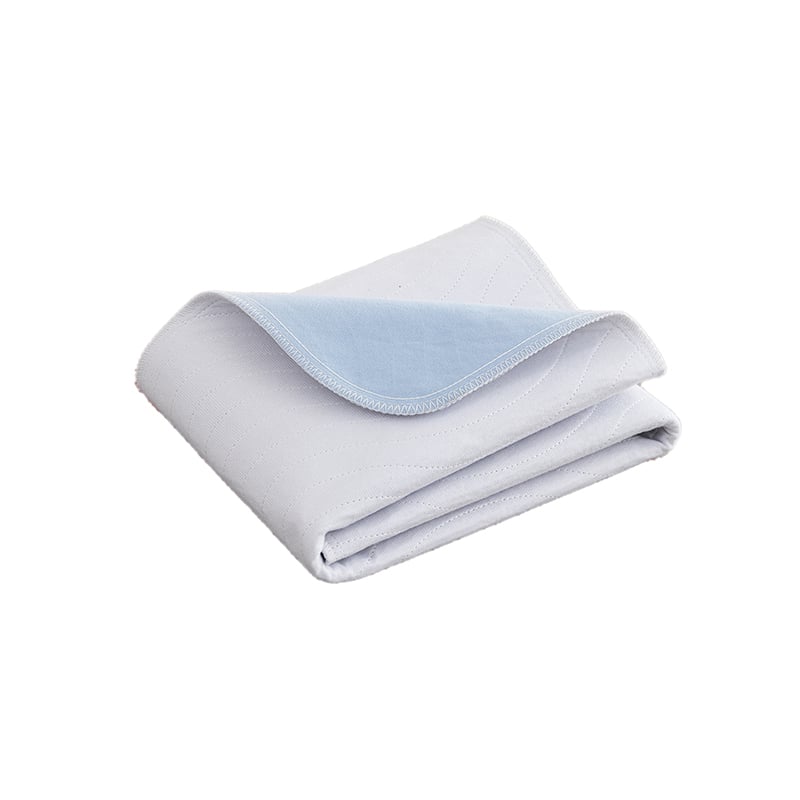
An underpad manufacturer plays a critical role in the healthcare, elder care, and hygiene product industries by producing absorbent protective pads designed to safeguard mattresses, bedding, and furniture from moisture, leakage, and contamination. These manufacturers combine advanced material science with precision engineering to deliver products that meet the demanding standards of hospitals, nursing homes, home care settings, and retail consumers worldwide. The core function of an underpad manufacturer is to design and produce layered absorbent pads that quickly draw moisture away from the surface, lock it within an absorbent core, and prevent it from leaking through to the surface beneath. This multi-layer construction typically involves a soft, skin-friendly top sheet, a highly absorbent pulp or polymer core, and a waterproof backing layer that creates a reliable moisture barrier. Leading underpad manufacturers invest heavily in research and development to refine each layer, improving absorption speed, capacity, and overall product integrity. Technologically, modern underpad manufacturers utilize superabsorbent polymer technology, which dramatically increases the liquid retention capacity of each pad compared to traditional fluff pulp designs. Many manufacturers also incorporate odor-neutralizing agents, anti-bacterial treatments, and hypoallergenic materials to enhance user comfort and hygiene. Automated production lines equipped with precision cutting, folding, and sealing machinery ensure consistent product quality at high output volumes, enabling manufacturers to serve both large institutional clients and individual consumers efficiently. The applications of products from an underpad manufacturer span a wide range of settings. In clinical environments, underpads protect patients with incontinence, post-surgical drainage, or limited mobility. In elder care facilities, they provide dignity and comfort to residents while reducing the workload on caregiving staff. In home care, they offer families a practical and cost-effective solution for managing incontinence or caring for bedridden individuals. Some manufacturers also produce underpads for veterinary use, maternity care, and even industrial surface protection, demonstrating the versatility and broad market reach of this product category.
Choosing the right underpad manufacturer gives you access to products that solve real, everyday problems without unnecessary complexity. Here is a straightforward look at the practical benefits that a reliable underpad manufacturer brings to the table. First, a dedicated underpad manufacturer focuses entirely on perfecting absorbent pad technology. This specialization means you get products built with purpose. Every layer, every material choice, and every production step is optimized for one goal: keeping surfaces dry and protected. You are not buying a generic product from a company that treats underpads as an afterthought. You are buying from a team that has spent years refining exactly what you need. Second, working with an established underpad manufacturer gives you access to consistent product quality. When you order in bulk for a hospital, a care facility, or a retail chain, you need every single pad to perform the same way. Reputable manufacturers run strict quality control checks throughout the production process, catching defects before products ever reach your hands. This consistency protects your reputation and reduces waste caused by product failures. Third, a capable underpad manufacturer can scale production to match your demand. Whether you need a small initial order to test a new product line or a large ongoing supply contract, manufacturers with modern automated facilities can adjust output without sacrificing quality. This flexibility saves you from the headaches of supply shortages or overstocking. Fourth, many underpad manufacturers offer customization options that let you tailor products to your specific requirements. You can work with the manufacturer to adjust pad size, absorbency level, backing material, and even packaging design. This means you can offer your customers or patients a product that fits their exact needs rather than forcing them to compromise with a one-size-fits-all solution. Fifth, sourcing directly from an underpad manufacturer typically reduces your per-unit cost compared to buying through distributors or resellers. Lower costs mean better margins for your business or more affordable pricing for your end customers. Manufacturers who operate efficient production lines pass those savings on to buyers, making high-quality underpads accessible at competitive price points. Sixth, a trustworthy underpad manufacturer stays current with regulatory requirements and safety standards. Products intended for medical or elder care use must meet specific certifications and compliance benchmarks. Working with a manufacturer who understands and actively manages these requirements protects you from liability and ensures the people using your products are safe. Seventh, strong manufacturers invest in sustainable production practices, offering eco-friendly materials and responsible waste management. If your brand values environmental responsibility, partnering with a manufacturer who shares those values strengthens your market position and appeals to a growing segment of environmentally conscious buyers. In summary, the right underpad manufacturer is not just a supplier. They are a production partner who helps you deliver reliable, safe, and cost-effective products to the people who need them most.

Tips And Tricks

Safe Sleep, Pure Protection: OEKO-TEX® Certified Waterproof Mattress Cover

18

Aug

Safe Sleep, Pure Protection: OEKO-TEX® Certified Waterproof Mattress Cover

View More
Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

11

Aug

Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

View More
Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

13

Mar

Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

View More
Bamboo vs. Cotton vs. Lyocell: Which Waterproof Mattress Protector Top Layer Is Right for You?

05

Aug

Bamboo vs. Cotton vs. Lyocell: Which Waterproof Mattress Protector Top Layer Is Right for You?

View More

Get a Free Quote

Our representative will contact you soon.
0/1000
Advanced Superabsorbent Technology That Keeps Surfaces Reliably Dry

Advanced Superabsorbent Technology That Keeps Surfaces Reliably Dry

One of the most important things to understand about a modern underpad manufacturer is the central role that superabsorbent polymer technology plays in product performance. Traditional absorbent pads relied primarily on fluff pulp to capture and hold liquid, but this approach had clear limitations. Fluff pulp can become saturated quickly, and once saturated, it tends to allow liquid to pool or leak under pressure, which defeats the entire purpose of the pad. A forward-thinking underpad manufacturer addresses this limitation by integrating superabsorbent polymers directly into the absorbent core. These polymers are capable of absorbing and retaining many times their own weight in liquid, converting free-flowing fluid into a stable gel that resists leakage even when the pad is compressed or shifted. This is a critical advantage in real-world use, where patients or residents move, turn, or apply body weight to the pad during extended periods of use. The practical impact of this technology is significant. For hospitals and care facilities, it means fewer pad changes per patient per shift, which reduces the workload on nursing staff and lowers the overall cost of consumable supplies. For home caregivers, it means greater peace of mind knowing that a single pad can handle larger fluid volumes without requiring immediate replacement. For patients and residents, it means less disruption, greater comfort, and reduced risk of skin irritation caused by prolonged moisture exposure. A skilled underpad manufacturer also engineers the distribution of superabsorbent polymers within the core to ensure even absorption across the entire pad surface, preventing the formation of wet spots in high-concentration areas. This uniform performance is a direct result of precise manufacturing processes and rigorous quality testing. Beyond absorption capacity, the best underpad manufacturers combine superabsorbent cores with fast-wicking top sheets that pull moisture away from the skin surface almost instantly. This two-stage performance, rapid surface wicking followed by deep core retention, is what separates a premium underpad from a basic one. When evaluating an underpad manufacturer, the sophistication of their absorbent core technology is one of the clearest indicators of overall product quality and long-term value.
Customizable Production Capabilities That Match Your Exact Specifications

Customizable Production Capabilities That Match Your Exact Specifications

A major competitive advantage offered by a professional underpad manufacturer is the ability to customize products to meet the precise requirements of different markets, care settings, and end users. Unlike purchasing pre-packaged products from a distributor, working directly with an underpad manufacturer opens the door to a collaborative development process where your specific needs drive the product design. Size is one of the most fundamental customization options. Underpads are used in a wide variety of contexts, from standard hospital beds and home mattresses to pediatric cribs, wheelchair seats, and examination tables. A versatile underpad manufacturer can produce pads in multiple dimensions to fit each application perfectly, eliminating the waste and inconvenience of oversized pads or the inadequate coverage of undersized ones. Absorbency level is another key variable. Light-duty underpads are appropriate for managing minor leakage or providing surface protection during medical procedures, while heavy-duty versions are designed for patients with severe incontinence or high-output drainage. An experienced underpad manufacturer can engineer the absorbent core to deliver the exact fluid capacity your application demands, ensuring you are not paying for more absorbency than you need or compromising with less than is required. Material selection also plays a major role in customization. The top sheet can be made from soft nonwoven fabrics for maximum skin comfort, or from more durable materials suited to repeated repositioning. The backing layer can be adjusted for different levels of waterproofing and grip, depending on whether the pad needs to stay firmly in place on a smooth hospital mattress or a textured home surface. Packaging and branding customization further extend the value of working with a dedicated underpad manufacturer. Private label programs allow healthcare distributors, retail brands, and institutional buyers to present products under their own brand identity, building customer loyalty and market differentiation. This end-to-end customization capability makes a capable underpad manufacturer a true strategic partner rather than just a commodity supplier.
Rigorous Quality Control Standards That Protect End Users and Your Brand

Rigorous Quality Control Standards That Protect End Users and Your Brand

Quality control is not a single step at the end of a production line. For a responsible underpad manufacturer, it is a continuous process woven into every stage of manufacturing, from raw material sourcing through finished product inspection and packaging. This commitment to quality is what separates manufacturers who consistently deliver reliable products from those who produce inconsistent results that create problems for buyers and end users alike. The quality assurance process at a reputable underpad manufacturer begins with the selection and testing of raw materials. Every batch of superabsorbent polymer, nonwoven fabric, fluff pulp, and backing film is evaluated against defined specifications before it enters the production process. This upstream control prevents defective or substandard materials from compromising finished products, which is far more efficient and reliable than trying to catch problems after manufacturing is complete. During production, automated monitoring systems track key parameters such as core weight, pad dimensions, sealing integrity, and backing layer adhesion in real time. Any deviation from established tolerances triggers an immediate alert, allowing production staff to identify and correct the issue before a large quantity of non-conforming product is produced. This in-process monitoring is a hallmark of a mature underpad manufacturer with a genuine commitment to consistency. Finished product testing adds another layer of assurance. Samples from each production batch are subjected to standardized absorption tests, leak resistance evaluations, and physical integrity checks. Results are documented and retained as part of a traceable quality record that can be reviewed by institutional buyers, regulatory auditors, or certification bodies. For products intended for medical or elder care use, compliance with relevant international standards and certifications is non-negotiable. A qualified underpad manufacturer maintains the documentation, testing protocols, and facility standards required to meet these benchmarks, protecting buyers from regulatory risk and giving end users confidence in the safety and performance of the products they rely on every day. This rigorous approach to quality is ultimately what builds long-term trust between an underpad manufacturer and its customers.