Trusted Underpad Supplier: High-Quality Absorbent Underpads for Healthcare and Home Care

application/underpad-supplier, application/underpad-supplier, 
Get a Quote
Get a Quote

underpad supplier

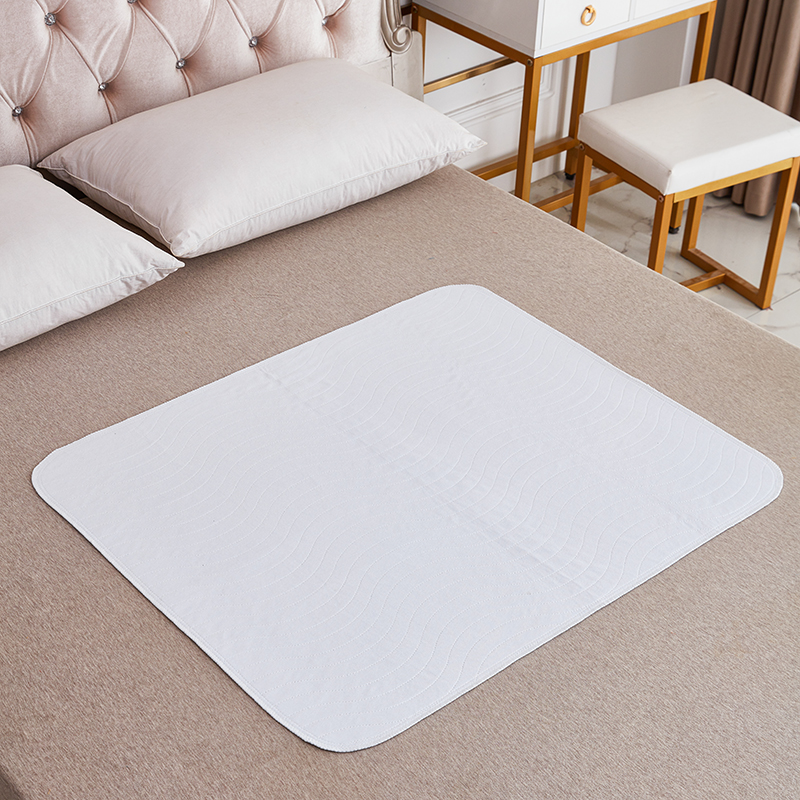
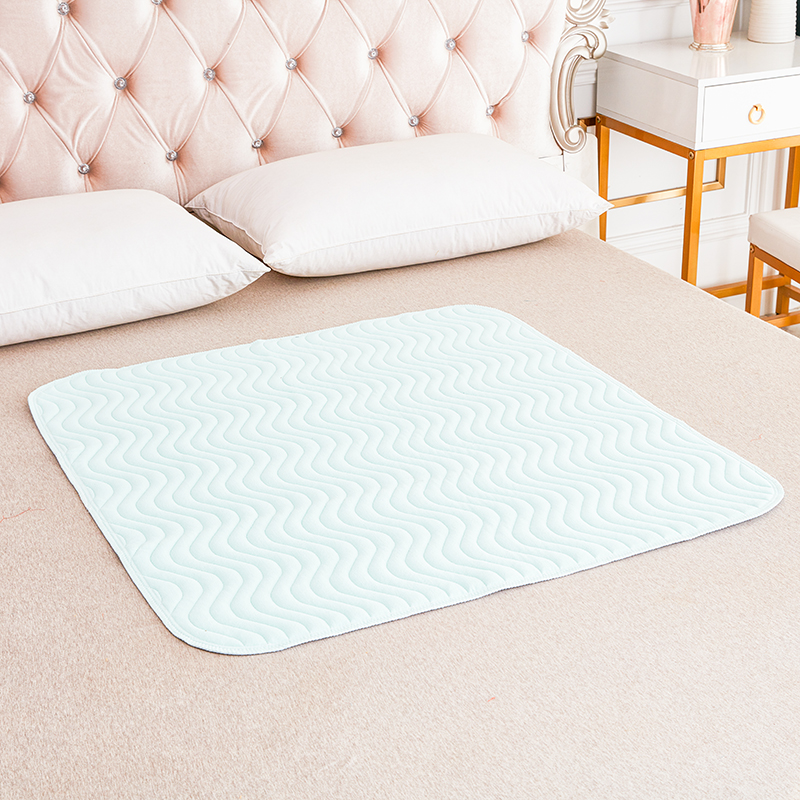
An underpad supplier plays a critical role in the healthcare, elder care, and hygiene product industries by providing high-quality absorbent underpads that protect patients, residents, and end users from moisture-related discomfort and skin damage. These suppliers source, manufacture, and distribute a wide range of underpads designed to meet the diverse needs of hospitals, nursing homes, home care settings, and retail consumers. The core function of an underpad supplier is to deliver products that effectively manage fluid absorption, keeping surfaces dry and reducing the risk of pressure ulcers, skin irritation, and infection. Modern underpad suppliers leverage advanced nonwoven fabric technologies, superabsorbent polymer (SAP) cores, and waterproof backing materials to engineer products that offer superior leak protection and rapid fluid acquisition. Technological features commonly found in products from a reputable underpad supplier include multi-layer construction, odor-neutralizing agents, soft top sheets for skin comfort, and reinforced edges that prevent bunching or shifting during use. Some underpad suppliers also integrate breathable backsheets that allow air circulation, reducing heat buildup and further protecting skin integrity. Applications for products sourced from an underpad supplier span a broad spectrum. In clinical environments, underpads are used on examination tables, operating surfaces, and patient beds to maintain hygiene and simplify cleanup. In long-term care facilities, they protect mattresses and bedding for residents with incontinence. Home care users rely on underpads supplied by trusted underpad suppliers to manage daily incontinence challenges with dignity and ease. Additionally, underpads find application in veterinary care, postpartum recovery, and even industrial settings where absorbent surface protection is required. A qualified underpad supplier also ensures regulatory compliance, offering products that meet international safety and quality standards such as ISO certifications and relevant medical device regulations. By partnering with a reliable underpad supplier, healthcare facilities and distributors gain access to consistent product quality, flexible order quantities, customizable specifications, and dependable logistics support that keeps supply chains running smoothly.
Choosing the right underpad supplier gives your business and your end users a set of practical, real-world benefits that make a measurable difference every single day. Here is a straightforward look at what a dependable underpad supplier brings to the table. First, a trusted underpad supplier delivers consistent product quality across every order. When you are managing a hospital ward, a nursing home, or a home care distribution network, you cannot afford variability. Consistent absorbency levels, reliable leak barriers, and uniform sizing mean your staff spends less time troubleshooting product failures and more time focusing on patient care. Quality consistency also reduces waste, because products that perform as expected are used fully rather than discarded due to premature failure. Second, a capable underpad supplier offers flexible production and order customization. Different markets and care settings have different requirements. Some facilities need extra-large underpads for bariatric patients. Others need underpads with a specific GSM weight for light incontinence management. A responsive underpad supplier works with you to adjust dimensions, absorbency grades, top sheet materials, and packaging formats so the final product fits your exact application without compromise. Third, working with an established underpad supplier gives you access to competitive pricing driven by economies of scale. Because these suppliers manufacture in volume and maintain efficient supply chains, they pass cost savings on to buyers. Lower per-unit costs allow distributors to maintain healthy margins while keeping retail prices accessible for end consumers, which drives higher sales volumes and stronger customer loyalty. Fourth, a reliable underpad supplier maintains robust inventory management and on-time delivery performance. Supply chain disruptions are costly in healthcare settings. A supplier with strong warehouse infrastructure, multiple production lines, and proactive logistics planning ensures you receive your orders on schedule, reducing the risk of stockouts that could compromise patient care. Fifth, reputable underpad suppliers invest in research and development, continuously improving their product formulations. This means buyers gain access to innovations such as enhanced SAP cores that lock away more fluid, softer nonwoven top sheets that reduce skin friction, and eco-friendly materials that align with sustainability goals. Staying ahead of product innovation through your underpad supplier keeps your product catalog competitive and relevant. Sixth, a professional underpad supplier provides full regulatory and documentation support. Certificates of conformity, material safety data sheets, test reports, and compliance documentation are readily available, simplifying the procurement process for regulated industries like healthcare and reducing the administrative burden on your purchasing team. Altogether, these advantages make selecting the right underpad supplier one of the most impactful decisions a healthcare distributor, retailer, or facility manager can make.

Practical Tips

Safe Sleep, Pure Protection: OEKO-TEX® Certified Waterproof Mattress Cover

18

Aug

Safe Sleep, Pure Protection: OEKO-TEX® Certified Waterproof Mattress Cover

View More
What is TPU?

11

Aug

What is TPU?

View More
Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

11

Aug

Jiangsu Etang Household Products Co., Ltd to Shine at 2025 Intertextile Shanghai Home Textiles Expo

View More
Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

13

Mar

Cheers to a Night of Milestones: Jiangsu Etang Celebrates a Year of Growth & Innovation

View More

Get a Free Quote

Our representative will contact you soon.
0/1000
Advanced Absorbency Technology That Keeps Patients Dry and Comfortable

Advanced Absorbency Technology That Keeps Patients Dry and Comfortable

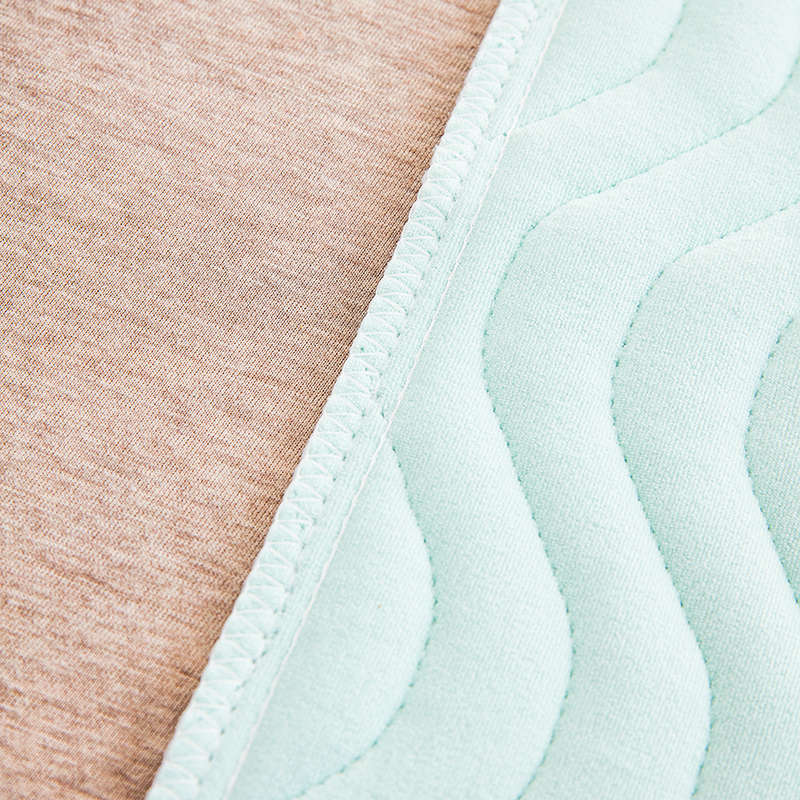
One of the most important qualities that defines a leading underpad supplier is the absorbency technology built into every product. At the heart of high-performance underpads lies a superabsorbent polymer core that rapidly draws fluid away from the surface and locks it deep within the pad structure. This mechanism is not simply about holding liquid. It is about doing so quickly enough to prevent pooling on the surface, which is the primary cause of skin maceration, pressure ulcer development, and general discomfort for patients and residents who spend extended periods in bed or seated. A top-tier underpad supplier engineers its products with a multi-layer system. The top sheet, typically made from soft nonwoven fabric, allows fluid to pass through instantly while maintaining a dry surface feel against the skin. Beneath it, a distribution layer spreads the incoming fluid evenly across the absorbent core, preventing localized saturation that would otherwise cause leaks. The SAP-infused core then absorbs and gels the fluid, holding it securely even under pressure. Finally, a waterproof polyethylene or breathable backsheet prevents any fluid from passing through to the mattress or surface below. What makes this technology particularly valuable is its performance under real-world conditions. Patients move, shift, and apply body weight to the underpad throughout the night. A well-engineered product from a quality underpad supplier maintains its integrity under these conditions, resisting rewet and keeping the skin environment dry. This directly reduces nursing workload, because fewer linen changes are needed and the risk of skin-related complications drops significantly. For healthcare procurement teams, sourcing from an underpad supplier that invests in absorbency technology means lower total cost of care, better patient outcomes, and stronger compliance with infection control protocols. The technology is not a luxury. It is a clinical necessity that every serious underpad supplier must deliver.
Customizable Specifications That Fit Every Care Setting and Market Requirement

Customizable Specifications That Fit Every Care Setting and Market Requirement

No two care environments are identical, and a forward-thinking underpad supplier understands that a one-size-fits-all approach simply does not serve the market well. Customization capability is a defining advantage that separates a truly professional underpad supplier from a basic commodity vendor. The ability to tailor product specifications to match the precise needs of a buyer is what enables long-term partnerships and sustained business growth. Customization from a capable underpad supplier starts with size. Standard underpads come in common dimensions, but many facilities require non-standard formats. Bariatric care units need wider and longer pads to provide adequate coverage. Pediatric wards may need smaller, lighter options. Veterinary clinics have entirely different dimensional requirements. A flexible underpad supplier maintains tooling and production capacity to accommodate these variations without imposing prohibitive minimum order quantities. Beyond size, absorbency level is another key customization parameter. Light, moderate, and heavy absorbency grades serve different clinical and consumer applications. A skilled underpad supplier works with buyers to select the right SAP loading, fluff pulp weight, and core thickness to achieve the target absorbency performance. Top sheet material selection is equally important. Soft spunbond nonwovens suit sensitive skin applications, while more structured materials may be preferred for industrial or veterinary use. Backsheet options range from standard polyethylene film to breathable laminate materials that improve comfort during extended wear or use. Packaging customization is another dimension where a professional underpad supplier adds value. Private label branding, custom carton sizes, retail-ready packaging, and bulk institutional formats all serve different distribution channels. A supplier that handles these requirements in-house reduces lead times and simplifies the supply chain for buyers. Ultimately, the customization capability of an underpad supplier is a direct reflection of its manufacturing maturity, engineering expertise, and commitment to customer success. Buyers who leverage this capability gain products that perform better in their specific context, strengthen their brand positioning, and build deeper loyalty among their end users.
Regulatory Compliance and Quality Assurance That Protect Your Business and Your Customers

Regulatory Compliance and Quality Assurance That Protect Your Business and Your Customers

In the healthcare and hygiene product industry, regulatory compliance is not optional. It is the foundation upon which trust is built between an underpad supplier, its distribution partners, and the end users who depend on these products every day. A serious underpad supplier invests heavily in quality management systems, third-party testing, and documentation infrastructure to ensure that every product leaving its facility meets or exceeds the applicable standards for safety, performance, and environmental responsibility. Quality assurance at a reputable underpad supplier begins at the raw material stage. Incoming nonwoven fabrics, superabsorbent polymers, adhesives, and backsheet films are tested against defined specifications before they enter production. This upstream control prevents defective inputs from compromising finished product quality and reduces the risk of costly recalls or customer complaints downstream. During production, statistical process control methods monitor key parameters such as absorbency capacity, tensile strength, seal integrity, and dimensional accuracy. Finished goods undergo final inspection protocols that include visual checks, functional testing, and packaging verification before shipment. From a regulatory standpoint, a compliant underpad supplier maintains certifications relevant to its target markets. ISO 9001 quality management certification demonstrates systematic process control. ISO 13485 certification is relevant for suppliers serving medical device markets. Products destined for European markets require CE marking where applicable, while those entering North American healthcare channels must meet FDA registration requirements for medical devices. An underpad supplier that proactively manages these certifications removes a significant compliance burden from its buyers, who can present documentation to their own customers and regulatory bodies with confidence. Environmental compliance is an increasingly important dimension of the underpad supplier relationship. Buyers in sustainability-conscious markets expect suppliers to demonstrate responsible sourcing, reduced plastic content, and adherence to chemical safety standards such as REACH and RoHS. A progressive underpad supplier addresses these expectations through material innovation and transparent supply chain reporting, giving buyers the documentation they need to meet their own corporate sustainability commitments. Partnering with a compliance-focused underpad supplier is ultimately a risk management decision that protects your business reputation, your customer relationships, and your ability to operate in regulated markets without interruption.